

What buyers should verify first
CNC cost rises when a drawing forces extra setups, long flexible tools, slow finishing passes or excessive inspection. DFM should happen before design freeze and again before fixtures or production tooling are committed.
| Review area | What good control looks like | Buyer action |
|---|---|---|
| Deep narrow pocket | Long tools chatter and cut slowly | Open geometry or reduce depth |
| Sharp internal corner | Rotary cutters require a radius | Use the largest functional radius |
| Thin wall | Clamping and cutting cause distortion | Thicken or support |
| Tight tolerance everywhere | Extra finishing and inspection | Limit to CTQs |
| Multiple orientations | More fixtures and datum transfer | Consolidate access |
1. Design around tool access
Visualize how a rigid cutter reaches each surface. Increase internal radii, avoid extreme depth-to-width ratios and provide clearance around walls and bosses. A deep pocket with a tiny corner radius forces a slender cutter and smaller cuts. Increase the radius where the mating component allows, and check that the holder clears adjacent walls. Compare the revised toolpath time with the original instead of assuming every geometric simplification saves the same amount.
2. Reduce setup count
Features machined from different directions require refixturing, datum transfer and verification. Align features where function allows. Four mounting holes that can be reached from the same face may share one setup. Moving one hole to the underside introduces another clamping operation and datum transfer. Keep the change only if the assembly benefit justifies that extra work.
3. Treat walls and floors as structures
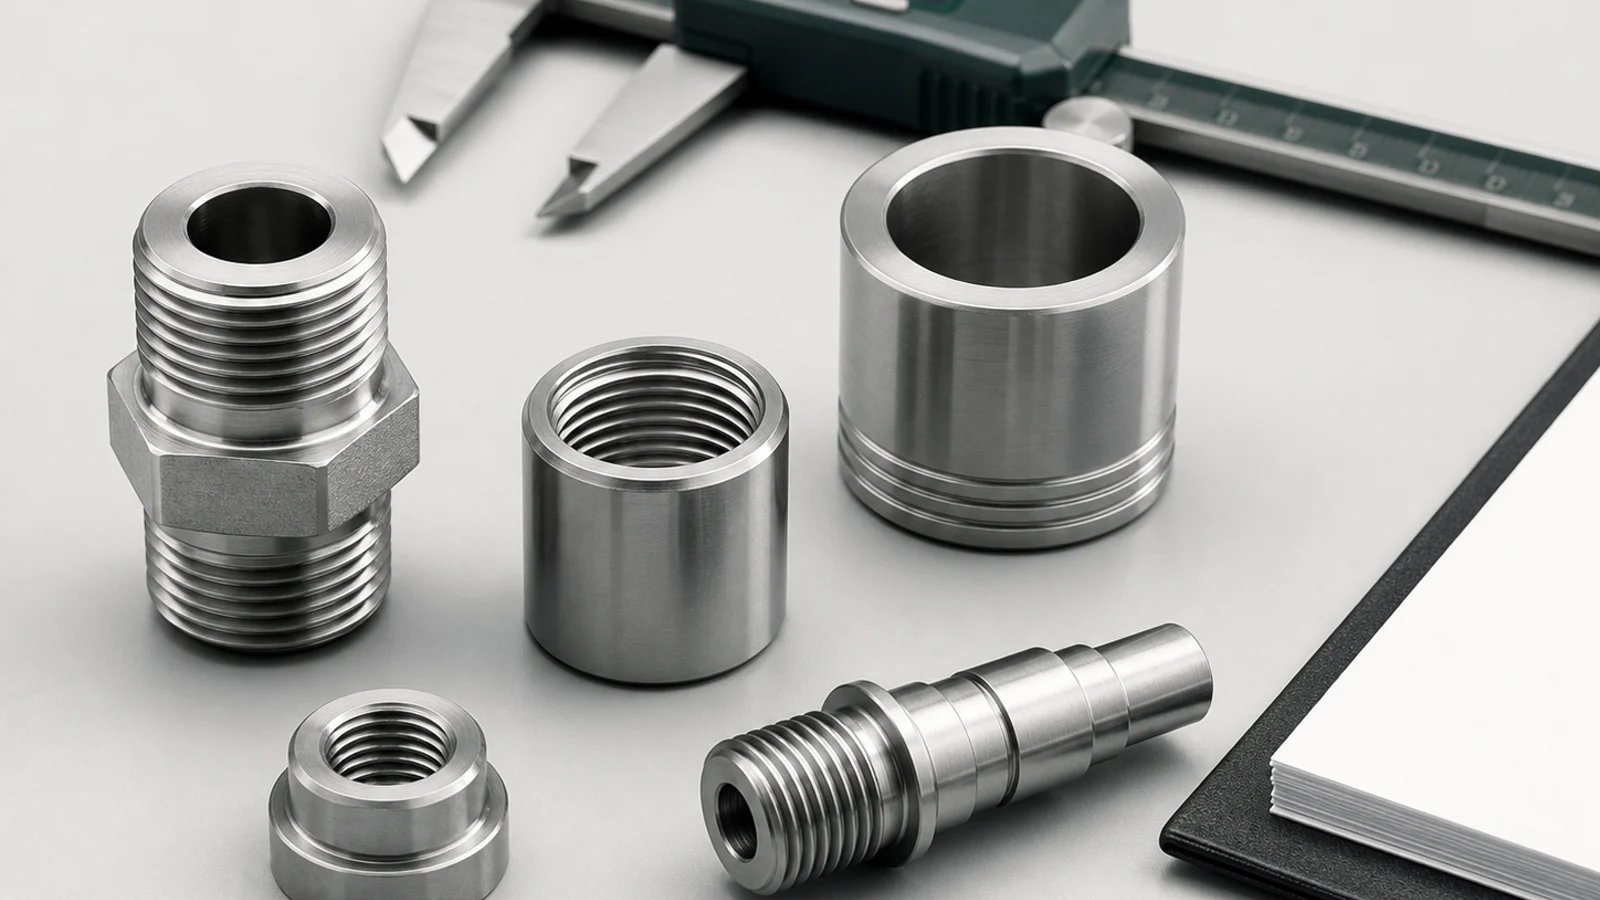
Thin sections move under clamp force, heat and residual stress. Add ribs, increase thickness or sequence roughing and stress relief. A 1 mm wall surrounding a deep cavity can deflect even on an accurate machine. Leave support material during roughing, use balanced removal and finish with a documented clamping strategy. Inspect after release from the fixture to reveal springback.
4. Use standard details
Standard hole sizes, thread forms, corner radii and stock thicknesses reduce special tools and procurement delays. Confirm the preferred hole sizes with the actual shop because tool availability varies. A standard thread with unusual full-depth requirements can still need a special tool or extra clearance. Specify usable engagement and allow the normal drill point where function permits.
5. Separate function from appearance
Identify cosmetic faces, allowable tool marks, grain direction, protected threads and post-finish dimensions instead of demanding premium finish everywhere. Mark visible faces on the drawing and agree sample-based limits for tool marks and handling defects. A hidden mounting surface often needs flatness and cleanliness without cosmetic polishing. Reducing its appearance requirement saves money only if it removes an actual finishing or inspection operation.
6. Omitting the material condition
Name the grade, temper or heat-treatment condition and product form. A callout of aluminum leaves the supplier to choose properties that may not match the design. Changing material after a first article can invalidate cutting data, finish appearance and mechanical assumptions.
7. Leaving edges undefined
Specify which edges need an edge break and which sealing or locating edges must stay sharp. An unspecified deburr instruction can create either harmful burrs or excessive rounding. Use a measurable limit where the edge affects assembly and an approved visual sample where it is cosmetic.
8. Confusing drilled depth with thread engagement
State the usable full-thread length and allow room for tool lead and chips. A blind hole drilled exactly to the required engagement depth cannot usually provide that much complete thread. Review tap-drill depth, drill point and bottom clearance together.
9. Choosing datums that cannot locate the part
Select datums that represent how the component locates in its assembly and can be simulated during inspection. A flexible unfinished wall may make a poor primary datum. Review manufacturing and inspection access before adding a demanding position tolerance.
10. Ignoring the assembled tolerance stack
Check how individual dimensions accumulate across a housing, cover and bearing spacer. Three dimensions each permitted ±0.05 mm can contribute ±0.15 mm in a simple worst-case linear stack. Allocate variation to the features that actually control the functional gap, using the appropriate stack method.
11. Designing deep holes without an evacuation route
A long small-diameter hole can require special drills, controlled coolant and slower cycles to remove chips. Ask whether the hole can be shortened or approached from another face without compromising alignment. Record the revised process and inspection method if two drilling directions are proposed.
12. Creating abrupt changes in wall thickness
Heavy bosses next to thin floors can release residual stress unevenly as material is removed. Blend section changes and preserve support where the design allows. Ask the shop to review the roughing sequence and inspect the free-state shape before finalizing the tolerance.
Why a larger internal radius can reduce price
Consider a deep pocket designed with a 1 mm internal corner radius. The shop may need a 2 mm diameter cutter with long reach, shallow step-down and several finishing passes. Increasing the radius to 3 mm can permit a 6 mm cutter that is substantially stiffer and removes more material per pass. On an illustrative batch, reducing pocket cycle time from 18 minutes to 11 minutes cuts seven machine minutes per part before setup and inspection are considered. The actual price effect depends on the machine rate and batch size, so request a side-by-side quotation rather than treating the example as a guarantee.
Practical buyer scenario
Changing a deep rectangular pocket to include larger corner radii can allow a shorter, stiffer end mill and faster material removal without changing enclosure function.
Topic-specific review checklist
- Material grade, condition and acceptable equivalent
- Functional datums and tolerance stack
- Minimum internal radii and accessible tool directions
- Thread engagement rather than unnecessary full depth
- Wall-thickness and distortion risk
- Deburring, edge-break and cosmetic zones
- Inspection evidence for the true CTQs
Frequently asked questions
When should DFM happen?
Before the design is frozen and again before production tooling or fixtures are committed.
Does a looser tolerance always reduce cost?
Only when it changes the process, inspection or scrap risk; discuss the actual feature.
Why are deep holes expensive?
Chip evacuation, tool deflection, peck cycles and special drills add time and risk.
What files help DFM?
A native or neutral 3D model plus a controlled 2D drawing with CTQs and notes.
Sources and further reading
Discuss this drawing requirement with WEKO before releasing material or committing the production route.