

What buyers should verify first
A useful factory audit follows one real order from quotation to shipment. Documents, operators, material, machines and inspection results should tell the same story.
| Review area | What good control looks like | Buyer action |
|---|---|---|
| Legal identity | License name matches quotation, invoice and bank beneficiary | Photo plus registry check |
| Production | Machines, tooling and scheduling are under direct control | Live walkthrough and machine list |
| Quality | Drawing revision, calibration and inspection records are traceable | Sample job traveler |
| Capacity | Quoted lead time matches loaded hours and bottlenecks | Capacity plan |
| Continuity | Backup machines, tools and material sources exist | Contingency record |
1. Verify who will manufacture the parts
Match the company name across the business license, quotation, contract, bank account and shipping paperwork. Ask for a live, unscripted walkthrough from incoming material to final inspection. A broker is not automatically unacceptable, but the commercial model must be disclosed. Record which site will perform milling, turning and final release, including any leased or partner equipment. A transparent trading company can be useful when it controls these interfaces; undisclosed outsourcing prevents a meaningful capability assessment.
2. Follow one real work order
Select a completed part and trace its drawing revision, material lot, program, setup sheet, in-process checks, final report and packing label. A connected record trail is stronger evidence than a wall of certificates. Ask the operator to retrieve the approved file without assistance from sales. If the traveler identifies revision C but the inspection report identifies revision B, follow the discrepancy to its disposition. Keep a redacted example of the connected records rather than collecting unrelated blank forms.
3. Test measurement capability
Bring one characteristic that matters to your assembly. Ask which instrument measures it, its resolution, calibration status, fixturing method and sampling frequency. Compare the method with the tolerance and datum scheme. For a bearing bore, ask for the master used to set the bore gauge and a demonstration on a retained part. Review repeatability across operators, not just the smallest displayed increment. A measurement system that cannot resolve the acceptance decision cannot validate production.
4. Challenge the schedule
Then ask what happens if a spindle, tool or finishing vendor fails.
5. Use a controlled trial order
Start with parts that expose the important risks, not only the easiest geometry. Freeze the revision, acceptance method, sample size and corrective-action deadline in writing before production. Include the hardest feature and the intended finish, even if that makes the pilot slightly larger. Require a marked drawing and results that identify the actual sample pieces. Resolve deviations before approving the process for repeat production.
6. Request evidence before the visit
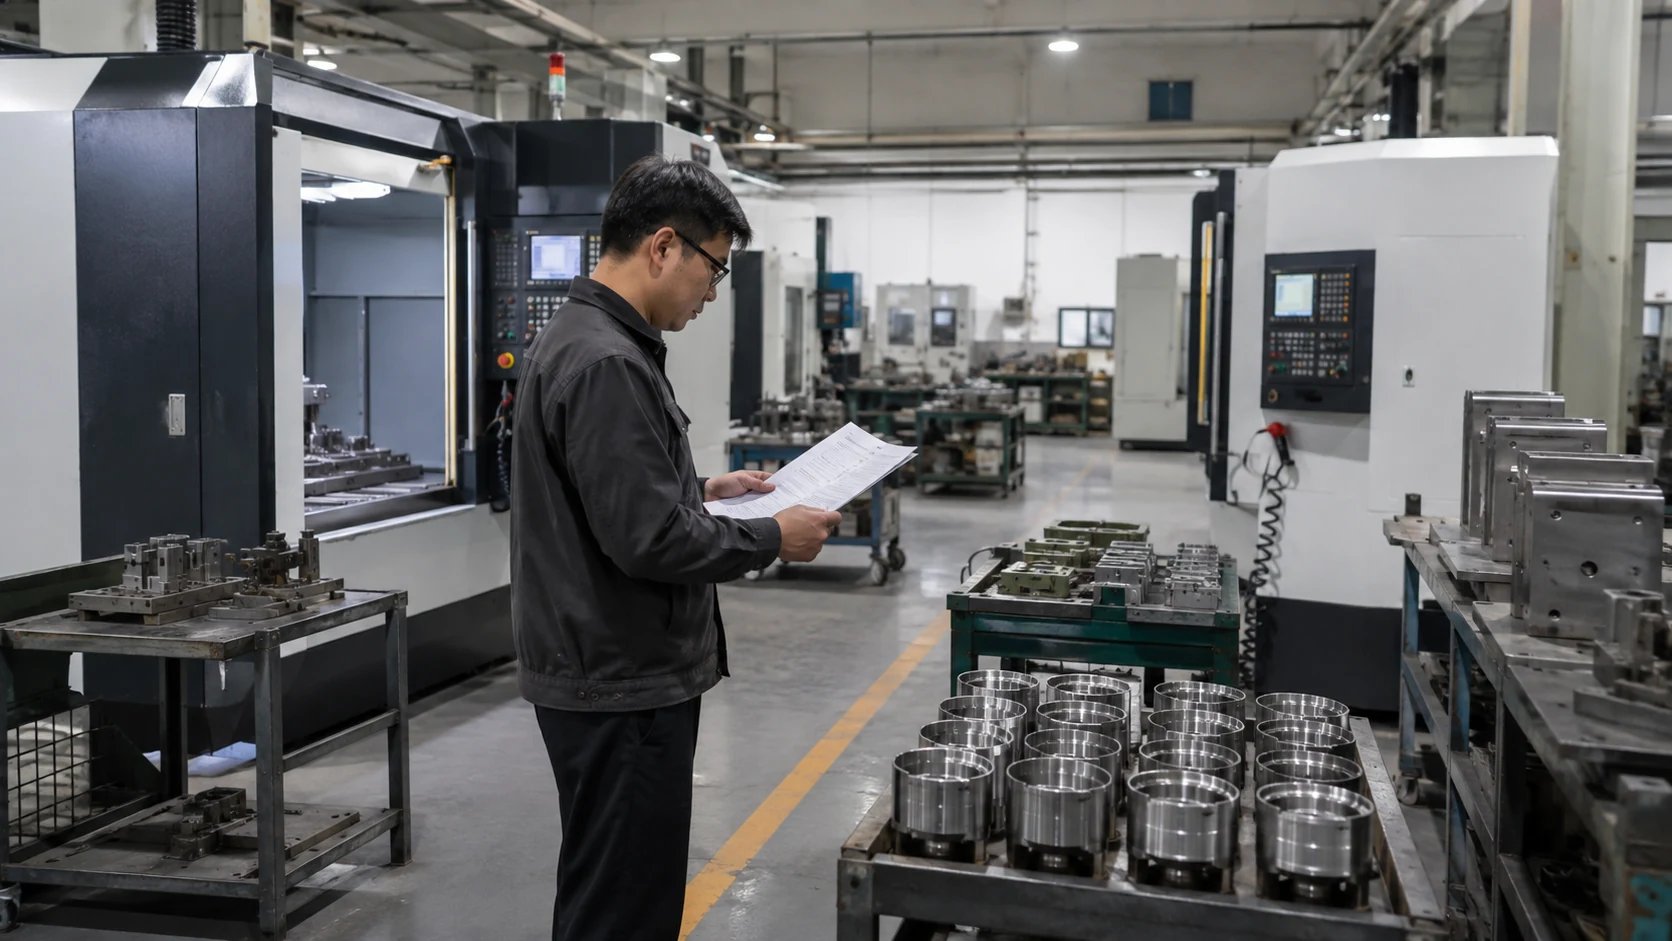
Ask for the machine list, process flow, organization chart and a redacted inspection report. Select a representative job to follow before arriving so the visit has a clear purpose. Missing documents are an audit finding to resolve, not a reason to substitute more marketing photographs.
7. Verify calibration records
Choose a gauge seen on the shop floor and match its identifier to the calibration record. Review range, uncertainty, due date and any restrictions on use. Ask how the shop assessed earlier shipments when a gauge last failed calibration.
8. Test material traceability
Pick one cut blank and follow its container label back to the stock heat and certificate. Then follow the same identity forward into machining and finished packing records. A certificate folder is inadequate if the physical material cannot be linked to it.
9. Observe housekeeping and handling
Look for segregation of accepted, rejected and unchecked parts, plus protection of finished surfaces. Open coolant spills, chips in packing areas or mixed bins can reveal weak process discipline. Record observed conditions and discuss the control that should prevent recurrence.
10. Interview the quality manager
Ask who can stop a shipment and who can authorize rework or request a customer concession. Follow one closed nonconformance through root cause and effectiveness evidence. A revised instruction without subsequent production evidence is an incomplete corrective action.
11. Verify backup capacity
Identify the alternate machine and confirm its tooling, workholding, program and inspection readiness. A nominally similar machine does not prove that a transfer is qualified. For an outside finisher, ask how an alternate source would be approved before urgent work moves there.
12. Agree release and change controls
Put the inspection scope, report format and approval gates in the trial order. Define notification requirements for material, route and subcontractor changes. Close each audit finding with an owner, due date and the evidence required before expanding the order.
Practical buyer scenario
For a motor housing, the buyer should audit bore measurement, concentricity setup, anodizing allowance, thread protection and lot traceability. A passing cosmetic sample is not enough if the bearing fit is the real failure mode.
Topic-specific review checklist
- Audit agenda and requested documents
- One representative work order and drawing revision
- Calibration and material-traceability samples
- Capacity evidence for the quoted process
- Corrective-action example with effectiveness check
- Written trial-order acceptance plan
Frequently asked questions
Can a remote audit replace an on-site audit?
It can screen suppliers and verify many records, but high-risk or regulated programs may still require an independent or on-site audit.
Should I reject a trading company?
No. Reject undisclosed outsourcing or weak control. A transparent integrator can be useful; a hidden handoff creates risk.
What should I request before the audit?
Machine list, certificates, organization chart, sample inspection report, calibration list, process flow and two customer references.
What is the best final test?
A paid pilot order with drawing-specific inspection and traceability requirements.
Sources and further reading
Discuss this drawing requirement with WEKO before releasing material or committing the production route.